Inner Bore Laser Hardening Optics for ID Surfaces

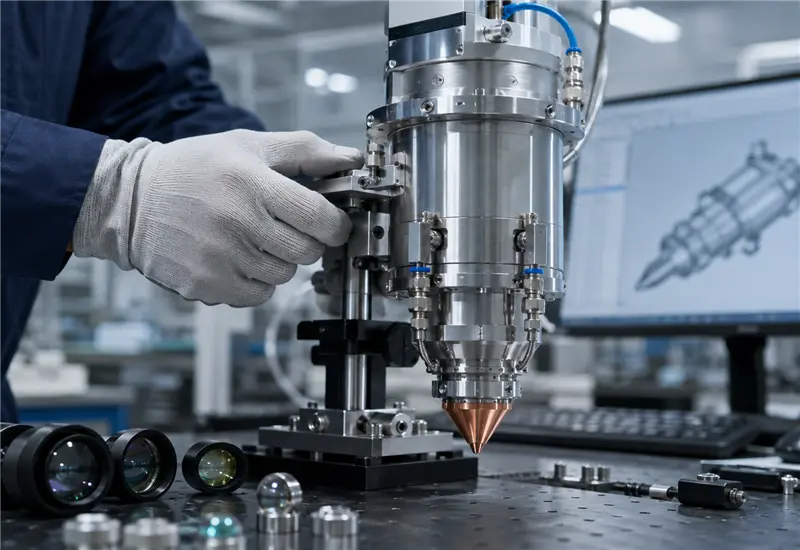
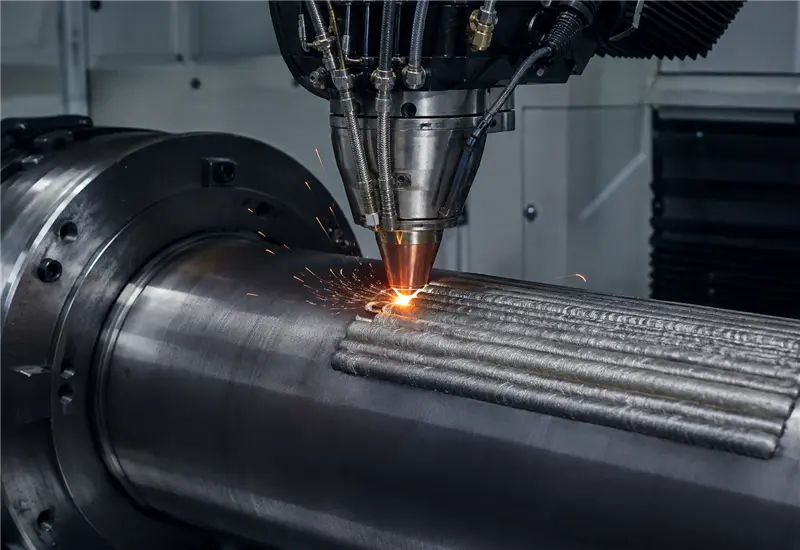
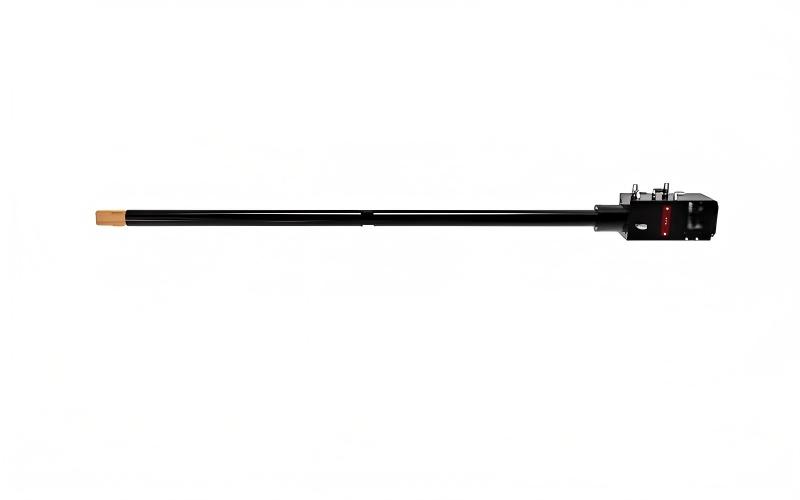
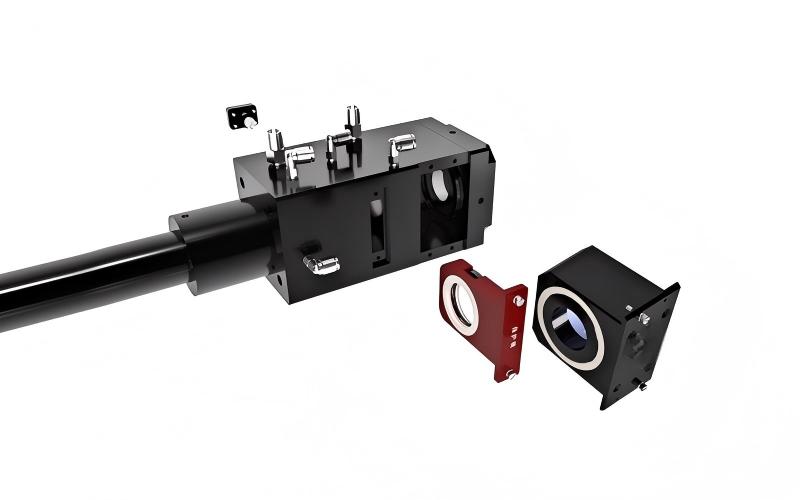
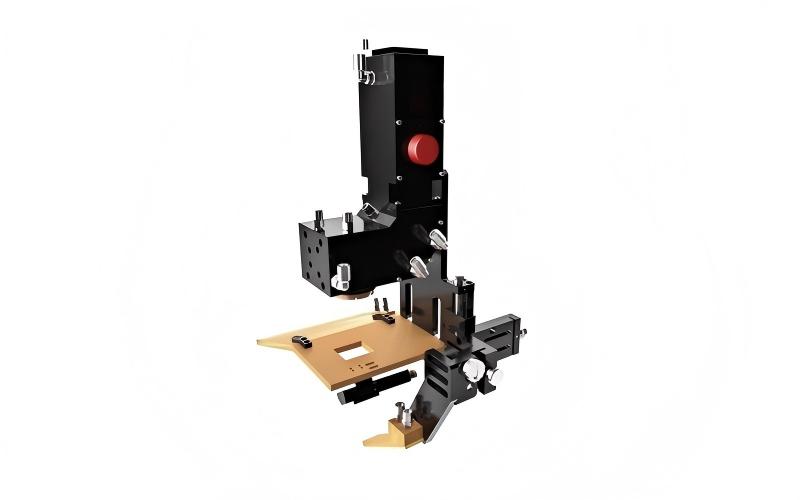
The Laser Hardening Head for Internal Surfaces is specifically designed for laser hardening of internal bores and cylindrical inner surfaces. Featuring a wide-beam configuration, the beam width can be freely adjusted from 4 mm to 30 mm, enabling both full-surface and selective area hardening for a wide range of industrial applications. With highly concentrated laser energy and a minimal heat-affected zone, the process requires neither water cooling nor oil quenching. No tempering treatment is required after hardening, significantly simplifying the production process. The laser hardening operation maintains the original dimensions and surface roughness of the component while preserving its overall mechanical properties. This technology delivers high-precision, low-distortion internal surface strengthening, making it ideal for wear-resistant and high-performance engineering components.
  • Spot Quality

    Uniformity into a circular shape uniformity of energy distribution directly affects
    Variable Beam Laser Hardening Head
  • Intelligent Control and Monitoring

    Lens temperature, molten pool CCD vision,temperature, powder flow monitoring
    Variable Beam Laser Hardening Head
  • Material Compatibility

    Copper alloy and Titanium alloy, Iron-based, Nickel-based, Cobalt-based and other metal powders
    Variable Beam Laser Hardening Head
  • Modular Design

    The lens system, moritoring system and optical path system operate in a modular manner,making them easy to disassemble, maintain and service
    Variable Beam Laser Hardening Head
  • Functionality

    High-efficiency water cooling,spatterresistant,
    dustproof, water mist-resistant, low spare parts replacement, frequency sealing rating( e.g., IP65)
    Variable Beam Laser Hardening Head
  • Safety

    Equipped with high-temperature alarm, real-time protection of equipment stability and workpiece cladding quality.
    Variable Beam Laser Hardening Head

Technical Parameters

Model Performance Parameters
Power Options 6KW
Fiber Interface QBH
Spot Size 2*20
Outer Dimension(mm) 1300*80*80 
Working Distance(mm) ~18
Operating Wavelength(nm) 1080
Cooling Type Water cooling
Water Quality Requirements Pure water

Application scenario

Internal bores of hydraulic cylinders requiring increased wear resistance and longer service life.

Inner surfaces of bearing housings, bushings, and sleeves for improved hardness and fatigue strength.

Valve bores, pump housings, and mechanical cavities requiring localized laser hardening.

Internal sealing surfaces of oil & gas, chemical, and power equipment to reduce wear and extend maintenance intervals.

Precision inner diameters of molds, dies, and tooling components requiring minimal distortion and high dimensional accuracy.

Tubular and hollow components requiring selective internal surface hardening with low heat input and excellent process stability.

FAQ

Q1: Can this laser hardening head perform both full-surface and selective area hardening on internal bores?

A1: Yes. The wide-beam configuration allows the beam width to be freely adjusted from 4 mm to 30 mm, enabling both full-surface hardening and selective area hardening on internal cylindrical surfaces. This

flexibility is ideal for components requiring targeted wear protection —  such as hydraulic cylinder barrels, pipe interiors, and precision bores — without hardening unnecessary areas.

Q2: Why does laser hardening with this head require no water cooling, oil quenching, or post-hardening tempering?

A2: Unlike conventional induction or flame hardening, this head delivers highly concentrated laser energy with a minimal heat-affected zone (HAZ) . The rapid self-quenching effect of the surrounding base material

eliminates the need for external quenching media or water cooling. No tempering treatment is required after hardening, significantly simplifying production while preserving the component’s original dimensions,

surface roughness, and overall mechanical properties.

Application Video

Products
Wide Track Laser Cladding Optics for OD Surfaces (1)
Wide-Track Laser Cladding Optics for OD Surfaces

Wide-track laser cladding optics for OD shafts, pipes and flat parts, using off-axis gravity powder feed with powder utilization up to 98%.
Annular Powder Fed Laser Cladding Head for OD Components (1)
Annular Powder-Fed Laser Cladding Head for OD Components

Annular powder-fed cladding head for cylindrical OD parts, delivering stable circular deposition, over 90% powder utilization and carbide layers up to 70 HRC.
Off Axis Wire Fed Laser Cladding Head for OD Repair (1)

Off-Axis Wire-Fed Laser Cladding Head for OD Repair
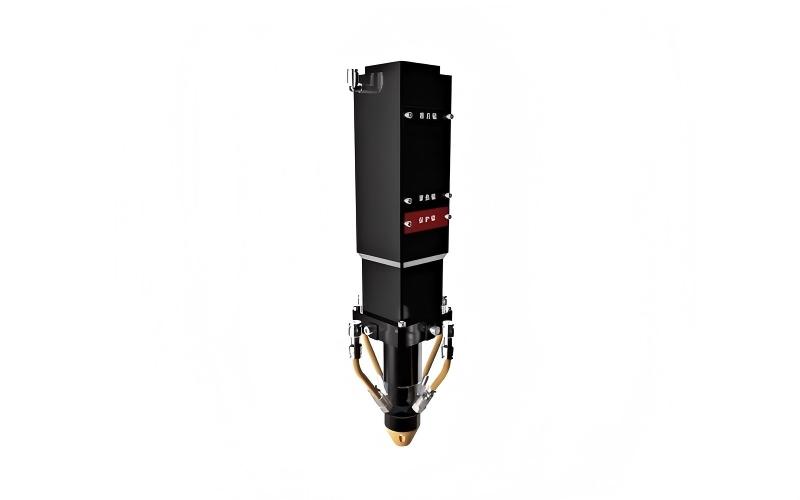
Wire-fed laser cladding head for OD repair and surface buildup, with 100% filler utilization, low distortion and compatibility with multiple alloy wires.
Four Jet Coaxial Powder Laser Cladding Head (1)

Four-Jet Coaxial Powder Laser Cladding Head
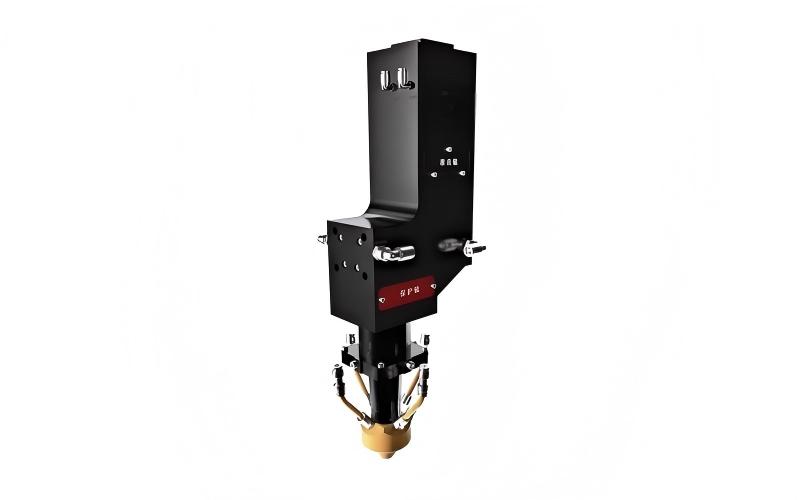
Four-jet coaxial powder head for multi-directional laser cladding on OD and complex surfaces, combining stable deposition with powder utilization of at least 90%.
Flat Top Square Beam Laser Cladding Optics for OD Surfaces (1)
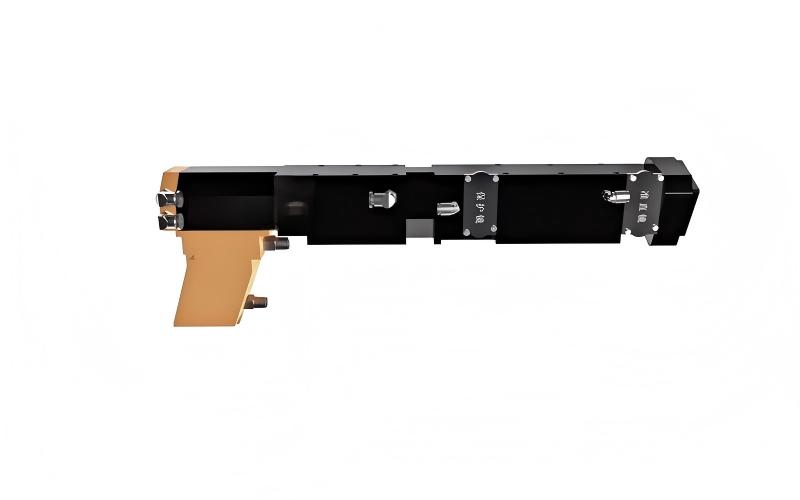
Flat-Top Square Beam Laser Cladding Optics for OD Surfaces

Square flat-top beam optics for OD laser cladding, designed for even energy distribution, high coating flatness and powder utilization of at least 90%.
Wide Track Inner Bore Laser Cladding Head (1)

Wide-Track Inner Bore Laser Cladding Head

Wide-track inner bore cladding head with a uniform rectangular beam and off-axis material feed, achieving powder utilization of at least 95% for ID surfaces.

Recent news

Laser Quenching of Gears A Paradigm Shift in Surface Strengthenin

Laser Quenching of Gears: A Paradigm Shift in Surface Strengthening

Aug 5, 2026
The mechanical transmission industry is undergoing a significant transformation. As high-end equipment moves toward lightweight designs and extreme precision, traditional hardening methods are reaching their physical limits. This report analyzes the transition from conventional induction quenching to laser quenching technology highlighting its technical advantages and economic impact.
READ MORE
case1

How to Select a Laser Cladding Head for Internal Bore Applications

Apr 22, 2026
Selection depends on bore diameter, processing depth, working distance, laser power, spot geometry, material delivery and heat-management requirements.
READ MORE
LZ

Powder-Fed vs. Wire-Fed Laser Cladding: Key Selection Factors

Apr 22, 2026

Compare deposition flexibility, material utilization, surface geometry, process stability, feedstock availability and integration requirements before choosing powder or wire.
READ MORE

See Latest Service

Application & Process Evaluation

We evaluate the workpiece, base material, target coating and production requirements to define a practical laser cladding route and equipment configuration.
LEARN MORE

Custom Optical Head Design

Custom processing heads and beam-shaping optics for internal bores, external surfaces, powder-fed deposition, wire-fed deposition and laser hardening.
LEARN MORE

Cladding Process Development

Parameter development and sample testing focused on deposition efficiency, dilution, coating quality, dimensional control and repeatability.
LEARN MORE
contact man

Contact us

    Products
    Contacts
    WhatsApp
    Email